What’s the Difference Between Single-Axis and Multi-Axis Torsion Bar Double Servo Press Brakes? Torsion Bar Double Servo Press Brake

Hey folks, if you’re in the metal bending game—whether you’re a small fab shop cranking out custom brackets or a mid-sized manufacturer knocking out panels for appliances, construction, or automotive parts—you’ve probably heard the terms “single-axis” and “multi-axis torsion bar double servo press brakes” thrown around. As someone who’s been selling these bad boys for years, I get it—sometimes the tech jargon gets so thick it’s hard to tell what actually matters for your day-to-day work. Most guys I talk to don’t care about the engineering details for the sake of it; they want to know which one will make their bends faster, more consistent, and less likely to mess up a $500 sheet of stainless steel. Let’s break this down like we’re grabbing a coffee and chatting shop, no stuffy whitepapers here.
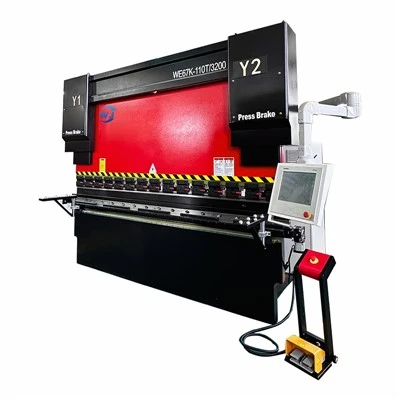
First, let’s start with the basics: what even is a torsion bar double servo press brake, anyway? If you already know this, skip ahead, but I’ll keep it quick for the new folks. Unlike old hydraulic press brakes that leak fluid, eat up electricity when you’re not using them, and sound like a jet taking off every time they bend a part, double servo press brakes use two servo motors (one on each side of the press beam) to drive the ram up and down. The “torsion bar” part? That’s a long, heavy steel bar that connects the two sides of the ram system, acting like a leveler. When the left side pushes, the torsion bar twists just enough to make sure the right side moves the exact same distance—no lopsided bends, no wonky gaps at the back of the die. That’s a huge step up from single servo press brakes that only use one motor to drive both sides, right? Wait, no—wait, the “single-axis” vs “multi-axis” part isn’t about the servos, it’s about the axes of motion for the backgauge and the ram’s upper tooling. Got it? Good, let’s dive into the real differences.
Single-axis torsion bar double servo press brakes are the entry-level workhorses, the ones that show up to job sites and fab shops that do mostly simple bends. The key here is “single-axis”—every moving part that positions the material or adjusts the tooling moves along just one straight line, no fancy synchronized motions. The backgauge, for example, has just a couple of axes total: usually the X-axis (how far back it sticks to hold the sheet) and maybe a Y-axis for up and down, but that’s only to adjust for different material thicknesses, not to get into tricky bends. Wait, no—single-axis means the backgauge can only move along one primary path, right? Let’s make that concrete. If you’re bending a simple L-shaped bracket, 12 inches long, 1/8 inch thick aluminum, all you need is the backgauge to slide back 3 inches, and the ram to drop 90 degrees. A single-axis press brake does that in its sleep. The torsion bar does its job, so the ram stays perfectly level the whole time—no more manually shimming die blocks to fix that left-right bend error you get with old hydraulics.
But here’s the catch with single-axis: it’s only good for simple stuff. Let’s say you’re bending a U-channel, where you have two bends 4 inches from each end. On a single-axis press brake, you can set the backgauge to go back 4 inches, bend, then flip the part over, set it back 4 inches the other way, bend again. That works, but it’s two extra steps, and flipping parts on a 10-foot sheet of steel is a recipe for scratched material, especially if it’s polished stainless. Now, what if you need a complex part, like a cabinet door with a hem on the top and bottom, and a 15-degree bend on the left side that’s offset from the main bend line? Single-axis can’t do that easily—you’d have to program it to move the backgauge up and sideways at the same time, but it’s not synchronized. The motion is janky, you have to babysit the machine, and you’ll get variations if the material isn’t perfectly flat.
Now, multi-axis torsion bar double servo press brakes. These are the ones for guys who do high-mix, low-volume or high-volume complex parts, like automotive trim, HVAC ductwork, or aerospace brackets. The “multi-axis” here means every moving part has multiple independent, synchronized axes—we’re talking 5, 7, even 12 axes on some of our top-of-the-line models. Let’s stick to the backgauge first, because that’s where most of the action is. A multi-axis backgauge has X, Y, Z axes, sometimes even R for rotating and W for widening. So if you need that U-channel, you can program the backgauge to first go back 4 inches, bend the first leg, then automatically move back another 8 inches, then slide left half an inch to account for the offset, then bend the second leg—all without touching the part. No flipping, no scratches, no extra labor.
The ram itself on multi-axis models also has axes, right? Wait, yeah—some multi-axis press brakes have crowning axes that adjust the height of the ram along its length, not just the torsion bar’s twist. So if you’re bending a 12-foot sheet that’s slightly warped, or if the die has a slight curve (for a rounded edge), the ram can automatically adjust each section of its upper tooling to match, so the bend is consistent end to end, no more thin gaps at one side or the other. That’s a game-changer for precision work. Another big one: speed and accuracy. Single-axis servo press brakes have a positioning accuracy of maybe ±0.005 inches, which is fine for simple parts, but multi-axis hits ±0.001 inches. For automotive parts that have to line up with a frame when assembled, that difference is the difference between a part that fits and one that gets sent back to the scrap bin.
Wait, let’s talk about speed, because everyone cares about that. Servo press brakes are way faster than hydraulics, but the axis count changes how fast you can run parts. Single-axis models have a bend speed of around 15-20 mm per second, which is fine if you’re doing 100 simple brackets a day. But multi-axis? Some of our models do up to 50 mm per second, because the backgauge and ram motion are synchronized. It’s not like the machine moves the backgauge, stops, moves the ram, stops, then moves the backgauge again—all that motion happens at the same time. For a complex part, that cuts cycle time by 30-50% compared to a single-axis machine. Let me give you a real example: last month, we had a customer in Chicago who makes metal display stands for retail stores. Before they got our single-axis model, they were making 20 display stands a day, each with 6 bends, taking 8 minutes per stand. After they upgraded to a 7-axis torsion bar double servo press brake, they’re making 35 stands a day, same quality, no extra workers. That’s real money—they just hired two new guys because they don’t have to do extra work on parts.
But wait, I’m not here to sell you a multi-axis machine if you don’t need it. A lot of fab shops come in thinking they need the biggest, baddest machine, and they end up overspending for nothing. Let’s talk about the tradeoffs, because single-axis isn’t obsolete. What are the pros of single-axis? First, price. A single-axis torsion bar double servo press brake is 20-40% cheaper than a multi-axis model, depending on the tonnage and bed length. If you’re a small shop with 2-3 guys doing mostly simple parts—like sign brackets, fence posts, or generic HVAC parts—you don’t need to pay for all those extra axes. Second, maintenance. More axes mean more parts to break, more sensors to calibrate. Single-axis machines are simpler, easier to fix if something goes wrong, and the spare parts are way cheaper. Third, operation. If you’re running a single operator who’s been doing this for 5 years, a single-axis machine is more intuitive—less programming, less setup, less chance of the operator messing up a complex axis sequence. I had a customer in Detroit last year, a one-man fab shop that does custom railings. He bought a multi-axis machine on a recommendation, and he ended up going back to single-axis because he hated programming all those extra axes. He only bends simple railing sections, so he was wasting time on features he never used. That’s a key point—match the machine to your workflow, not the other way around.
Now, what about the pros of multi-axis, beyond just complex parts? Let’s talk about repeatability. If you’re doing a 1000-part run, multi-axis will make every part exactly the same. Single-axis is good for runs up to, say, 500 parts, but after that, the backgauge can drift a little, the material can shift when you flip it, and you get variations. Multi-axis has linear encoders on every axis, so every position is measured in real time, and the machine adjusts automatically. That means no rework, no scrap from off-bends. Another pro: flexibility. A lot of our multi-axis models have quick-change tooling systems, so you can swap out dies and upper tools in under 5 minutes, compared to 20 minutes on a single-axis machine. That’s huge for job shops that get a new order every day, with different part sizes and bend requirements.
Wait, let’s clear up a common misconception I hear all the time: people think “single-axis” means only one servo motor, and “multi-axis” means multiple servos. That’s not true for torsion bar double servo press brakes. Both models have two servo motors, one on each side, connected by the torsion bar. The difference is how many axes of motion the backgauge and tooling have. So if someone tries to sell you a “single-axis double servo” that only has one motor? Run away—they’re mislabeling their machines. All our torsion bar double servo press brakes have two servos, and the torsion bar keeps the ram level regardless of axis count. That’s the whole point of this design, better than single-servo designs that can have tilt issues if one servo is slightly out of sync.
Let’s also talk about use cases to make this super clear. If you’re a small fab shop (1-5 employees), jobbing work mostly simple bends, runs under 500 parts, tight budget—single-axis is your guy. Examples: custom brackets, fence parts, basic HVAC duct, small sign components. If you’re a medium to large fab shop, jobbing complex parts, or high-volume production (runs over 1000 parts), need precision for assembly fit, do high-mix work—multi-axis is non-negotiable. Examples: automotive trim, appliance panels, aerospace brackets, retail display stands, large ductwork with offset bends.
Now, what about tonnage and size? Wait, that’s another question I get. Does a single-axis press brake come in high tonnage for thick steel? Yeah, we have single-axis models up to 300 tons, 12-foot beds, good for bending 1-inch thick steel beams for construction. Multi-axis models go up to 1000 tons, 20-foot beds, for heavy industrial parts. Tonnage doesn’t determine axis count—your part complexity and production volume do.
Let me throw in a real horror story to drive home the difference. Last year, a customer in Ohio had a job to make 2000 metal enclosures for electric vehicle chargers. Each enclosure had 8 bends, 4 of which were offset, so you couldn’t flip the part. They tried using a used single-axis press brake they’d bought cheap. The backgauge couldn’t move sideways while it moved back, so every third part was off by a quarter of an inch. They ended up with 300 scrap parts, lost $12,000 on the job, and had to rent a multi-axis press brake from us for the second half of the run. That’s the kind of headache you avoid by matching your machine to your work.
Another thing to consider: operator skill. If you hire young operators who are tech-savvy, can learn new software, a multi-axis machine is a win—they’ll get used to programming all those axes quickly, and they’ll be more productive. If you have veteran operators who’ve been bending metal for 20 years, don’t like fancy tech, a single-axis machine might be better because it’s less intimidating. You can get a lot of work done on a single-axis machine, no fancy degree required.
Wait, but what about energy efficiency? I mentioned earlier that servo press brakes are way better than hydraulics. Let’s compare single vs multi-axis here. Single-axis uses about 30% less energy than a hydraulic, multi-axis uses about 35% less, because the servos only use power when moving, unlike hydraulics that run nonstop to maintain pressure. So even if you pay more upfront for multi-axis, you’ll save on electric bills over time, especially if you’re running 8 hours a day, 5 days a week.
Now, let’s wrap this up so you don’t leave more confused than when you started. The key differences boil down to three main things: 1) Axis count and motion: single-axis has limited, linear backgauge/tooling motion for simple bends; multi-axis has synchronized, multi-directional motion for complex parts. 2) Accuracy and repeatability: single-axis is good for ±0.005 inch accuracy, fine for simple runs; multi-axis hits ±0.001 inch, perfect for precision, long runs. 3) Cost and flexibility: single-axis is cheaper, simpler, good for low-volume, simple work; multi-axis is more expensive, flexible, good for complex, high-volume work.
I know this is a lot, and every shop’s needs are different. If you’re sitting there thinking “I don’t know which one I need,” just reach out—we don’t push the most expensive machine, we push the machine that fits what you actually do. We’ve helped guys scale from single-axis to multi-axis when their business grows, and we’ve helped small shops save money by skipping the fancy features they don’t need. Whether you’re bending 10 brackets a week or 10,000 complex parts, we’ve got a torsion bar double servo press brake that’ll work for you.
Don’t let the tech jargon stress you out—just tell us what parts you make, how many a week, how complex they are, and we’ll walk you through the options. No pressure, no sales pitches, just straight talk about what’ll make your job easier and your shop more profitable. Hit us up whenever you want to chat, we’re here to help.
Pure Electric Servo CNC Bending Machine References:
- Metalforming Magazine. (2022). Servo Press Brake Technology: Trends, Capabilities, and Selection Guidelines.
- Fabricators & Manufacturers Association, International. (2023). Guide to Press Brake Selection for Custom and Production Metal Forming.
- Machine Design. (2021). Torsion Bar vs. Traditional Ram Leveling for Press Brakes.
- The Fabricator. (2022). How Axis Count Impacts Press Brake Productivity and Part Complexity.
Tianjin Wujia CNC Machine Tool Co., Ltd.
Tianjin Wujia CNC Machine Tool Co., Ltd. is one of the most reliable manufacturers and suppliers of torsion bar double servo press brake in China. As we have world-leading production equipment and strong manufacturing capabilities, we warmly welcome you to wholesale advanced equipment at competitive price from our factory. For more cheap products, contact us now.
Address: No. 8 Yonglian Road, Shuangtang High-end Hardware Products Industrial Park, Jinghai District, Tianjin
E-mail: leo@wujiamachine.cn
WebSite: https://www.wujiacncmachine.com/
